
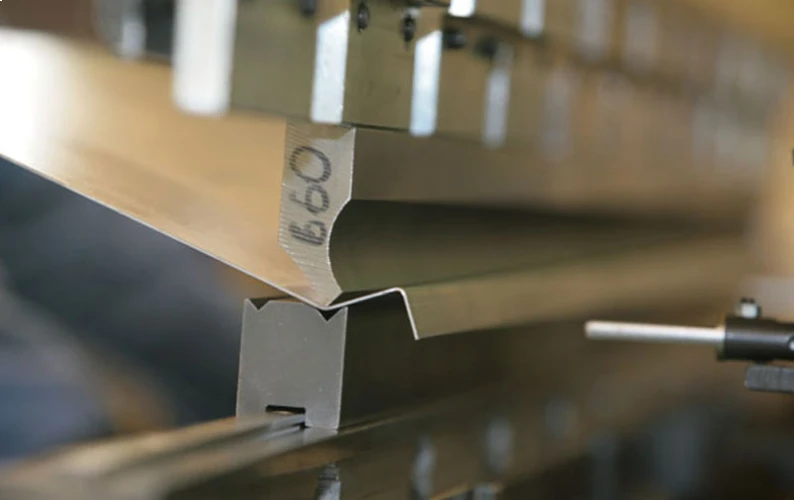
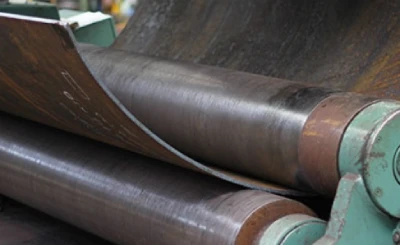
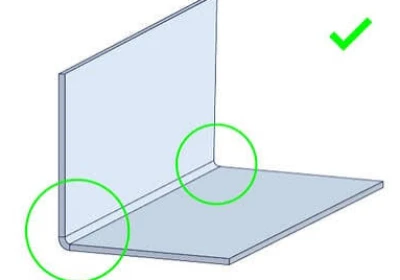
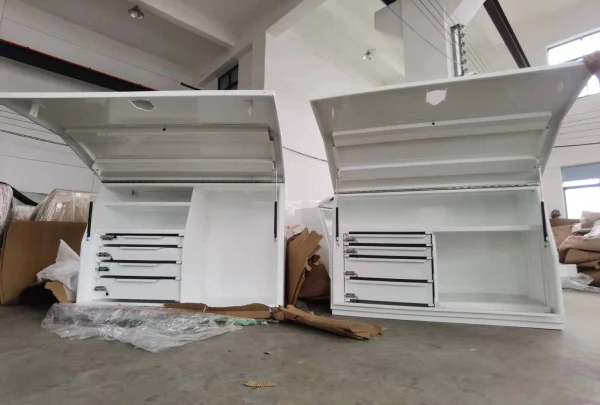
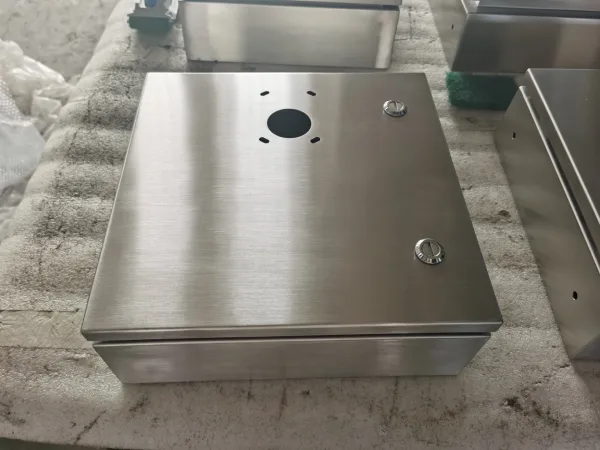
In the field of precision aluminum sheet metal bending, a fundamental principle holds true:Material selection is the primary determinant of process reliability and part performance. Common defects—cracking, inconsistent springback, and surface scratches—rarely stem solely from processing errors; they typically arise from mismatches between material properties and the process. Viewing the aluminum sheet metal bending process simplistically as metal forming is reductive; it is fundamentally the precise response of the material’s microstructure to complex stress states.
Therefore, in aluminum sheet metal bending, the bending design should not be built around existing sheet stock. Instead, rigorous analysis of the bend geometry, functional requirements, and material deformation characteristics is essential to select the optimal aluminum sheet metal bending material and heat treatment condition. This demands a deep understanding of how material properties—such as elastic modulus, yield strength, and elongation—directly determine springback and minimum bend radius.
This paper aims to provide professional procurement and engineering teams with a systematic material selection framework. It shifts the success of custom aluminum sheet metal bending from reliance on post-process adjustments to a data-driven, predictable material selection process. This ensures projects achieve a balance between performance, reliability, and total cost control.
Key Properties Analysis of Aluminum Sheet Metal Bending Material
A successful aluminum sheet metal bending process fundamentally relies on precise control of the material's stress-strain curve. Properties such as Young's modulus (E) and yield strength (σₛ) directly influence springback. Elongation (A%) and work hardening index (n-value) jointly define the material's ductility and strain distribution capability, determining the achievable bending radius or feasibility of complex multi-step forming. Plastic strain ratio (r-value) and surface condition are directly linked to dimensional consistency and surface quality control in mass production.
Elastic Modulus (E) of Aluminum Sheet Metal Bending Material
For all aluminum alloys, the elastic modulus E is a relatively constant value, approximately 69 GPa. This characteristic is the physical root cause of springback during custom aluminum sheet metal bending. During bending, energy stored in the material during the elastic deformation stage is released upon unloading, causing the workpiece angle to spring back.
Due to aluminum’s lower E value, it stores a proportionally higher amount of elastic strain energy compared to steel. Consequently, springback in aluminum sheet metal bending processes is more pronounced and must be precisely quantified. When planning custom aluminum sheet metal bending projects, Supro first performs initial springback simulations based on the E value to prevent issues like angular deviation and assembly failure.
Yield Strength (σ_s) of Aluminum Sheet Metal Bending Material
Yield strength is a critical variable for aluminum alloy materials, directly defining the stress threshold at which permanent plastic deformation begins. Yield strength values vary significantly across different aluminum sheet metal bending materials and temper conditions. For instance, 6061-T6 exhibits a yield strength around 275 MPa, while 5052-O may be below 90 MPa. Higher yield strength introduces two primary challenges: first, it increases springback during the aluminum sheet metal bending process, demanding more complex angle compensation; second, it limits the minimum bend radius.
Elongation (A%) of aluminum sheet metal bending material
Elongation represents the total plastic deformation a material can withstand before fracture, expressed as a percentage. It evaluates the forming limit of aluminum sheet metal bending material and is a decisive indicator of resistance to cracking on the outer bend surface.
When bending aluminum sheet metal with small inner radii (e.g., R < 1 times material thickness), the outer bend surface experiences extreme tensile strain. Materials with high elongation (e.g., 5052-O, which can achieve A% over 20%) can safely withstand this strain, whereas materials with low elongation (e.g., 6061-T6, where A% may be only 10%) are prone to cracking.
For custom aluminum sheet metal bending parts involving complex or severe forming requirements, the material’s elongation must be matched to the bending geometry specifications. A professional aluminum sheet metal bending manufacturer should provide minimum bend radius recommendations based on different elongation data as part of a design for manufacturability review.
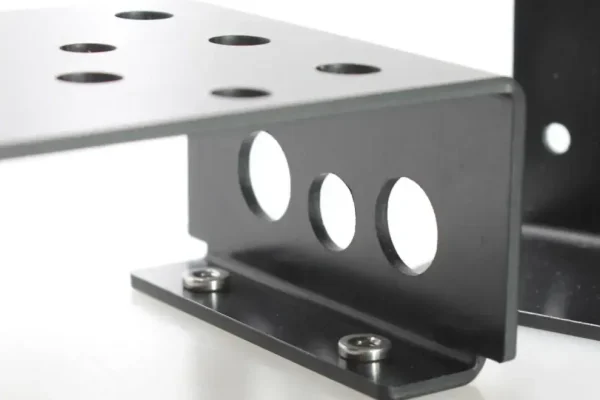
Work Hardening Index (n-value) of Aluminum Sheet Metal Bending Material
The work hardening index (n-value) describes the rate at which a material strengthens or hardens during plastic deformation. A higher n-value indicates that the aluminum sheet metal bending material can more effectively resist localized thinning through self-strengthening in the deformation zone, resulting in more uniform strain distribution. This property is critical for aluminum sheet metal bending parts requiring multi-pass progressive bending or featuring complex flange characteristics.
For example, some 5xxx series alloys (such as 5083) possess relatively high n-values, enabling excellent performance in complex forming operations. In aluminum sheet metal bending processes, understanding the n-value aids in predicting localized hardness increases post-bending and their impact on subsequent operations like punching or riveting. As a professional aluminum sheet metal bending manufacturer, Supro not only focuses on the material’s initial state but also anticipates changes during processing, ensuring consistent performance of the final part.
Plastic Strain Ratio (r-value) of Aluminum Sheet Metal Bending Material
The plastic strain ratio (r-value) measures the difference in a sheet’s deformation capability between its in-plane and thickness directions, revealing material anisotropy. An r-value unequal to 1 indicates inconsistent material properties across different orientations. In aluminum sheet metal bending, this leads to a critical issue: when the bend line is parallel or perpendicular to the sheet’s rolling direction, the bending angle and springback will differ.
For high-precision aluminum sheet metal bending of enclosures or structural components, this directional variation may cause assembly difficulties or shape distortion. Professional aluminum sheet metal bending manufacturers specify the orientation of the rolling direction on the part’s flat pattern and use consistent layup directions during production to control material anisotropy.
Surface Conditions of Aluminum Sheet Metal Bending Materials
Surface condition is a property directly affecting product aesthetics and functionality, making it highly significant in custom aluminum sheet metal bending. Common surface finishes include anodizing, powder coating, pre-painting, brushing, or mirror polishing. The primary risks when bending these materials are surface scratches, indentations, or coating cracks. This not only compromises appearance but may also damage the coating’s corrosion protection. Professional custom aluminum sheet metal bending solutions require specialized scratch-free bending dies, clean production environments, and optimized pressure control.
Bending Characteristics of Mainstream Aluminum Alloys
When selecting materials for custom aluminum sheet metal bending, understanding the inherent properties and bending limitations of mainstream alloys is critical. Different alloy series, such as the 5xxx and 6xxx series, exhibit fundamental differences in formability, strength, and post-processing capabilities. These differences directly impact the cost, performance, and delivery reliability of custom aluminum sheet metal bending parts. The table below analyzes the core bending characteristics, potential risks, and typical applications of each series from an engineering manufacturing perspective, providing a clear comparative framework.
Typical Grades and Conditions | Bending Characteristics | Risks and Countermeasures | Applicable Scenarios | |
1xxx Series (Pure Aluminum) | 1050-O、1100-H14 | Exceptionally high ductility, extremely low yield strength, minimal springback, enabling the completion of highly complex forming operations. | Low strength, prone to deformation: Parts exhibit poor rigidity after forming and are susceptible to accidental dents during handling. Countermeasure: Optimize packaging and logistics solutions. | Chemical containers, deep-drawn stamped parts, decorative interior trim, non-structural components requiring ultimate formability. |
3xxx Series (Manganese Series) | 3003-O/H14 | Good balance of formability and corrosion resistance, moderate strength, and suitable work hardening rate. | Hardness variation between batches: May cause slight changes in rebound. Countermeasure: Require material test reports (MTR) and conduct precise verification of the first article. | Heat exchanger fins and shells, building roofs, general-purpose enclosures, and cookware. |
5xxx Series (Magnesium Series) | 5052-O/H32、 5083-O | Excellent overall bending performance. O-temper exhibits good ductility; H32 and similar tempers provide practical strength while maintaining good formability. | H-tempered materials crack when bent at sharp angles: Strictly adhere to the minimum state-based bending radius (e.g., inner radius ≥1t recommended for 5052-H32). | Ship components, automotive body panels, outdoor electronic device enclosures, high-demand chassis parts |
6xxx Series (Magnesium-Silicon Series) | 6061-T4/T6 | The T4 condition is ideal for age-hardening, as bending followed by spray painting and baking significantly enhances strength. The T6 condition offers high strength but is virtually impossible to cold-bend. | T4 and T6 conditions are easily confused. Countermeasure: Clearly specify the condition on drawings and orders, and conduct random hardness inspections on incoming materials. | T4 Condition: Automotive collision structures and bicycle frames requiring post-weld strengthening. T6 Condition: Used exclusively for simple, large-radius structural support members. |
7xxx Series (Zinc-based) | 7075-T6 | Under conventional conditions, it is extremely difficult to cold bend, exhibiting extremely high strength but very low ductility, with a pronounced tendency toward brittleness. | Cold bending is highly prone to cracking. Countermeasure: When aluminum sheet metal bending is unavoidable, employ specialized processes such as hot forming and rigorously validate heat treatment procedures. | Aerospace frames, high-performance racing components, and other structures with extreme strength requirements and simple bending profiles. |
Only 4 steps
online custom metal fabrication parts
Contact our experts team and experience the efficiency and economic benefits of digital metal fabrication services.
Upload Design Files
STL , STEP (.stp), IGES (.igs), (.ZIP), or PDF.
Also be a sample or an idea
Quote & Design Analysis
Instant factory quotes and DfM reports, the most reasonable solution.
Manufacturing Begins
Digital processes can initiate order tasks within 24 hours.
On-Time Delivery
Keeping delivery promises, approved by 3000+ Global Company buyers.
Selection of Temper for Aluminum Sheet Metal Bending Material
In bending processes, the material temper—often denoted by suffixes O, H, or T—is a more critical selection criterion than alloy grade. It precisely describes the metallurgical history and microstructure prior to delivery, directly defining yield strength, ductility, and response to the aluminum sheet metal bending process. Misinterpreting the temper designation is thus the most common and costly error leading to batch process failures.
O Temper (Annealed)
O temper indicates the material has undergone full annealing, resulting in the softest and most stable microstructure. For aluminum sheet metal bending, O-temper material offers ultimate ductility and the lowest yield strength. Its low dislocation density and eliminated internal stresses enable it to withstand extreme plastic deformation during bending without fracturing.
Thus, O-temper is the preferred aluminum sheet metal bending material when your custom aluminum sheet metal bending part design involves sharp corners, extremely small inner bend radii (e.g., R/t < 0.5), or complex multi-bend configurations. Its extremely low yield strength also results in relatively small and more predictable springback.
However, this exceptional formability comes at the cost of reduced strength: the final structural rigidity of bent parts relies entirely on the limited strength increase achieved through work hardening. It is unsuitable for any load-bearing structural components and requires careful handling during subsequent transport and assembly to prevent impact deformation.
H-Temper (Strain-Hardened)
The H-temper is achieved through mechanical processing like cold rolling, inducing strain hardening to enhance strength. The subsequent numerical designation precisely describes the degree and method of processing. The H-temper represents the critical balance point between formability and initial strength. Taking the common 5052-H32 as an example: “H3” indicates strain hardening followed by stabilization treatment, while “2” signifies its strength is approximately one-quarter of the difference between the alloy’s fully hardened (H38) and annealed (O) states.
5052-H32 offers superior initial strength and dent resistance compared to the O condition while retaining sufficient ductility to complete 90-degree aluminum sheet metal bending. When selecting aluminum sheet metal bending material, it is essential to understand the performance differences between H1x (strain hardened only), H2x (strain hardened followed by partial annealing), and H3x (strain hardened followed by stabilization treatment). Precise specifications must be made based on part requirements for strength, formability, dimensional stability, and other critical factors.
T-Temper (Heat-Treated Condition)
The T-temper refers to the material condition after solution heat treatment and aging. Its selection requires careful consideration, as confusion regarding this condition ranks among the most costly errors in aluminum sheet metal bending. The T6 condition involves full artificial aging, achieving the alloy’s maximum strength but resulting in a sharp decline in ductility.
The vast majority of T6 material is unsuitable for demanding cold bending operations, as it is highly prone to microcracking during the aluminum sheet metal bending process. Unless the bending radius is exceptionally large (typically R/t > 5), designing cold bends for T6 material should be avoided.
Conversely, the T4 condition is achieved through heat treatment followed by natural aging. It retains good ductility, enabling complex cold bending operations. Following aluminum sheet metal bending, T4 material can undergo artificial aging via low-temperature baking at approximately 175°C-200°C, significantly boosting its final strength to levels approaching T6. This form-first, strengthen-later process path offers an excellent engineering solution for achieving high-strength, complex-geometry custom aluminum sheet metal bending structural components.
Material Selection Decision for Aluminum Sheet Metal Bending Process
Successful custom aluminum sheet metal bending projects involve far more than selecting an alloy grade from a chart. It requires progressively mapping part functional requirements into specific, actionable aluminum sheet metal bending material specifications. First, the part’s end-use environment must be clearly defined, encompassing mechanical loads, exposure conditions, thermal management needs, and industry-specific certification requirements.
For instance, high-magnesium 5xxx series alloys should be cautiously selected for welded structures to prevent solidification cracking, while 3xxx or 5xxx series with superior corrosion resistance should be prioritized in salt spray environments.
Second, quantitative analysis of geometry and bending difficulty becomes critical. Calculating the relative bend radius (R/t ratio) at key bends and comparing it against minimum bend radius data for different material conditions enables rapid feasibility assessment. For instance, a design with R/t < 1 necessitates high-ductility materials like 5xxx series O-temper or 6xxx series T4-temper. Simultaneously, springback effects in the aluminum sheet metal bending process must be evaluated: For multi-sided enclosed enclosures, material conditions with lower yield strength and more consistent springback should be selected to ensure assembly dimensions.
Finally, the final aluminum sheet metal bending material decision requires balancing performance, manufacturability, and cost. This involves comprehensive consideration of material unit price, scrap rate, secondary processing costs, and supply chain stability. For instance, replacing the difficult-to-process and costly 6061-T6 with 6061-T4 (post-bend coating reinforcement) is recommended. Alternatively, where strength requirements permit, the more economical and formable 5052-H32 is suggested.
Conclusion
Selecting the correct aluminum sheet metal bending material fundamentally establishes the foundation for stable part performance throughout its entire lifecycle. A systematic material selection framework—from defining functional requirements to analyzing geometric complexity, and then balancing performance with manufacturability—effectively prevents cracking, assembly failures, or overdesign caused by improper material choices.
If you require aluminum sheet metal bending services, contact us immediately! Supro is a professional aluminum sheet metal bending manufacturer. Leveraging advanced equipment, extensive manufacturing experience, and a specialized engineering team, we deliver flawless aluminum sheet metal bending services to over 3,000 companies worldwide, backed by genuine manufacturer pricing.
We possess deep expertise, technology, and cutting-edge equipment, understanding the demands and standards for sheet metal bending parts across industries including agriculture, healthcare, automotive manufacturing, and aerospace. Supro operates 12 distinct sheet metal bending machines, delivering one-stop sheet metal bending services across industries while ensuring high-quality products, professional customer service, and on-time delivery. If you have any questions or concerns about our sheet metal bending services, contact us immediately. We will proactively meet all your project requirements!