Progressive tooling and repeat-production stamping
Custom Progressive Die Stamping Services in China
Supro MFG supports progressive die projects from drawing review and strip-layout planning through tooling, trial parts and repeat production. Send your part drawings, material, annual volume and critical tolerances for a factory feasibility review.
Tooling to Repeat Production
One engineering path for DFM, die development, trial parts, production release and ongoing tool maintenance.
Process-Specific Quality Control
Control plans can cover strip feeding, pilot alignment, burr height, flatness, hole position and tool-wear monitoring.
Secondary Operations and Assembly
Tapping, welding, deburring, finishing and assembly can be coordinated around the approved stamping process.
Progressive Die Stamping Services
Supro MFG provides custom progressive die stamping for repeat-production metal parts, supported by die design and manufacturing, DFM review, trial parts, production stamping, tool repair and preventive maintenance. During the early project stage, our engineers review geometry, material, tolerances, annual demand and secondary operations to determine whether progressive tooling is the right manufacturing route. Prototype fabrication or simpler tooling may be recommended before production tooling when the design or demand is not yet stable.
One-Stop Progressive Stamping Manufacturer
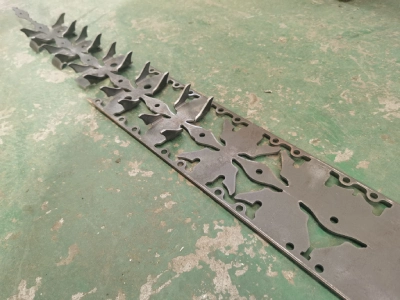
Progressive stamping can combine piercing, blanking, bending, forming and other operations in a controlled strip-fed sequence. We also review tapping, welding, deburring, surface finishing and assembly where the approved part design requires them. Typical candidates include electrical terminals and contacts, clips, brackets, mounting plates, washers, connector components and other repeat-production stamped parts. Tooling, process and inspection requirements are confirmed from the drawing rather than promised as a generic standard.
Progressive Die Stamping Material Solutions
1060
6061-T6 / T5
6063
5052-O
5083
5754
7075
2A12
201
303
304
316
316L
420
430
440
H62
H65
H68
H90
C10100
C11000
C12000
C51100
Q235 - F
Q255
16Mn
12CrMo
# 45
20 G
Corrugated Steel Sheets
Fluorocarbon color steel
Embossed panels
Galvanized sheet
Get a list of sheet metal materials
0.6mm - 200mm
1220mm × 2440mm
Custom rolls & strips
0.05mm - 300mm
1220mm × 2440mm
Custom rolls & strips
0.5mm - 6mm
1200mm × 4000mm
Custom rolls & strips
0.5mm - 500mm
1500mm × 6000mm
Custom rolls & strips
- Aluminum alloy
- brass
- Pure copper
- bronze
- steel
- Spring steel
- Carbon steel
- Galvanized steel
- Fluorocarbon Color Coated Sheet
- Stainless steel
- Titanium alloy
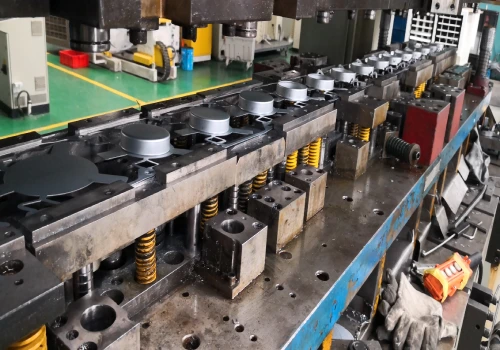
Multi-Station Progressive Tooling
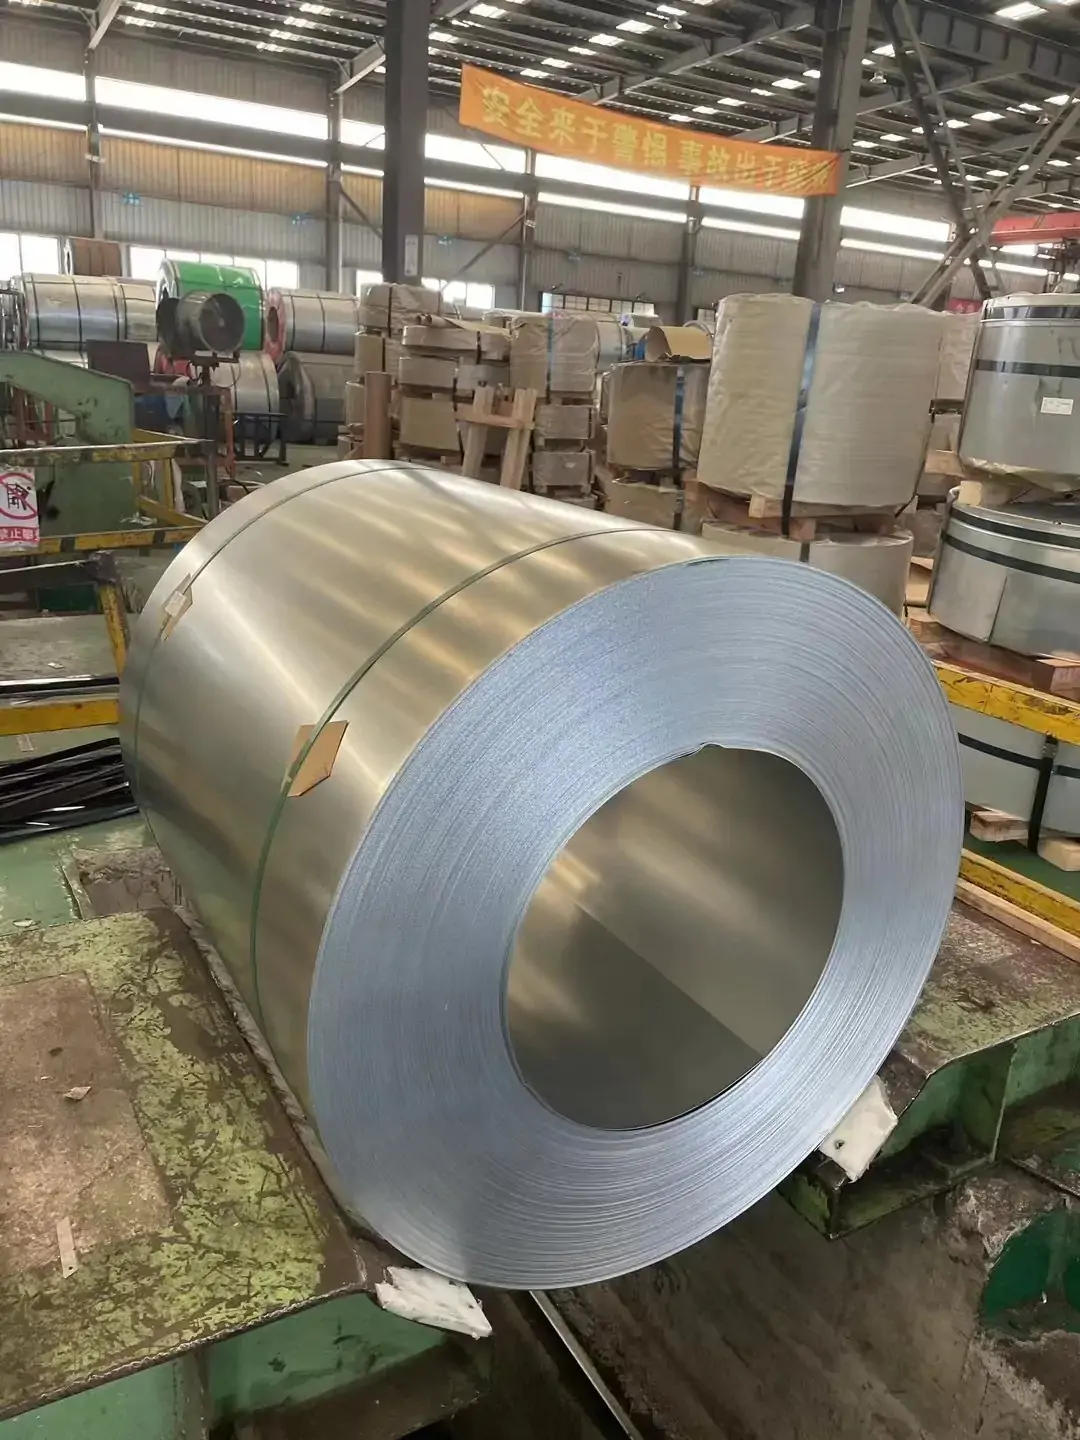
Coil and Strip Material Supply
Why Choose Supro MFG for Progressive Die Stamping
Progressive stamping combines automated feeding, multiple forming stations and controlled inspection to support repeat-production parts. Supro MFG reviews strip layout, material utilization, tooling life, quality documentation and secondary operations so the manufacturing plan matches the drawing and purchase requirements.
- Production efficiency: Progressive dies combine automated strip feeding with sequential stamping stations for stable repeat production.
- Multiple operations: Piercing, blanking, bending, forming, coining and other approved operations can be integrated into one tooling sequence.
- Material utilization: Strip layout and part orientation are reviewed to reduce avoidable scrap while protecting carrier strength and feeding stability.
- Automation and process control: Operators focus on feeding, press conditions, in-process inspection and tool monitoring rather than repeated manual handling.
- Flexible manufacturing support: Prototype fabrication, production tooling, tool repair, secondary operations and assembly can be planned around the project stage.
- Quality planning: PPAP, FMEA, APQP, control plans, FAI and related records can be supported when required by the customer and agreed before quotation.
- Consistent production: Pilot alignment, die clearance, burr height, flatness, hole position and tool wear are monitored according to the approved control plan.
- Cost review: Tooling investment and piece price are evaluated together against annual volume and alternative processes.
What Is Progressive Die Tooling?
A progressive die is a multi-station stamping tool. Coil or strip material advances through a controlled sequence of stations, with each press stroke completing operations such as piercing, blanking, bending, forming, embossing or coining. The strip carrier, pilots and feed progression maintain part position until the finished component is separated. Tool design, die clearance, station balance, material behavior and maintenance planning all affect production stability and part quality.

DFM and Quality Controls for Progressive Stamping
Engineering review follows the drawing, material and production risk—not a generic checklist.
Before tool release
Engineering and tool review
Before tool release, engineering review should address material grain direction, bend radius, station sequence, carrier strength, strip utilization, springback, slug control and access for inspection. Where requirements are still changing, we may recommend prototype fabrication or soft tooling before committing to a production die.
Review focus: grain direction · bend radius · station balance · strip utilization · inspection access
During production
Production quality controls
During production, controls may include incoming material verification, first-article inspection, pilot and feed alignment, burr-height monitoring, flatness and hole-position checks, in-process sampling, final dimensional inspection and documented tool maintenance. Required reports are agreed before quotation.
Control focus: feeding alignment · die clearance · burr height · FAI · dimensional and material reports
Related capability: custom metal stamping services
Industries and Repeat-Production Applications
Progressive stamping supports repeat-production OEM programs. Every part still requires project-specific engineering, quality and documentation confirmation.
Terminals, contacts, connectors and shielding components
Brackets, retainers and repeat-production stamped components
Clips, plates and mounting parts for equipment assemblies
Telecom hardware, brackets and enclosure components
Renewable energy
Conductive, structural and mounting hardware for energy systems
Standard parts and fasteners
Controlled-repeat components for stable ongoing demand
Engineering Resources and Process Selection
Use these guides to compare process fit, tooling economics, material options and production risks before requesting a quotation.
Process selection
Choose the process before committing to tooling
Quality and production
Plan controls around part risk and repeatability
Material options
Check forming behavior and sourcing constraints
Verified project cases will be added only when the part function, material, thickness, annual volume, process challenge, inspection method and measurable result can be documented.
Progressive Die Stamping FAQ
It is normally considered when repeat demand, stable part design and multiple operations can justify dedicated tooling. The break-even point depends on geometry, material, tool complexity, annual volume and alternative process costs.
Yes. Prototype fabrication or simpler tooling may be recommended to validate geometry and function before a production die is released.
Tool ownership, storage, preventive maintenance, repair, replacement inserts and engineering-change responsibilities should be defined in the quotation and purchase agreement.
Provide 2D or 3D drawings, material and temper, thickness, annual quantity, batch size, critical tolerances, burr direction, finishing, required documents and target timing.
Depending on project requirements, documents may include material certificates, FAI, dimensional inspection records, control plans, PPAP elements and production inspection reports.
Tapping, welding, deburring, finishing and assembly can be reviewed as part of the approved manufacturing plan.