For OEM procurement directors and mechanical design engineers, optimizing sheet metal fabrication spending requires striking a balance between upfront capital expenditures (CapEx) and long-term operating costs (OpEx).
During the early stages of product development, flexible sheet metal fabrication techniques—particularly the combination of CNC fiber laser cutting and multi-axis press brake forming—offer an ideal, low-risk solution.
These “soft tooling” processes eliminate non-recurring engineering (NRE) costs and can accommodate rapid engineering change orders (ECOs). However, as production volumes scale up to high EAU (estimated annual usage) levels, relying solely on flexible sheet metal fabrication processes—which are constrained by cycle times and indirect costs associated with equipment downtime—makes it impossible to sustain unit cost floors.
Navigating this transition presents a critical strategic decision: it is essential to accurately determine when to phase out flexible sheet metal fabrication and transition to hard tooling, such as progressive or composite stamping dies. Although stamping processes require substantial upfront tooling investments (US$10,000–100,000+), integrating complex piercing, blanking, and coining into a stamping cycle lasting less than one second can effectively reduce the variable cost per unit.
To achieve sustainable production scalability, a mathematically rigorous break-even analysis is required—assessing raw material strip utilization, press tonnage requirements, and die amortization to determine the exact threshold at which hard dies offer a competitive advantage in terms of total cost of ownership (TCO).
Core Sheet Metal Fabrication Process Mechanisms: Laser Cutting/CNC Bending vs. Metal Stamping
Evaluating process dynamics in precision sheet metal fabrication requires comparing flexible soft tooling workflows with efficient hard tooling. CNC laser cutting and press brake forming enable rapid setup with no new product development (NRE) costs, while progressive die stamping integrates complex geometries into a single press cycle, thereby achieving unparalleled cost optimization.
Laser Cutting and CNC Press Brake Forming (Agile, Low NRE)
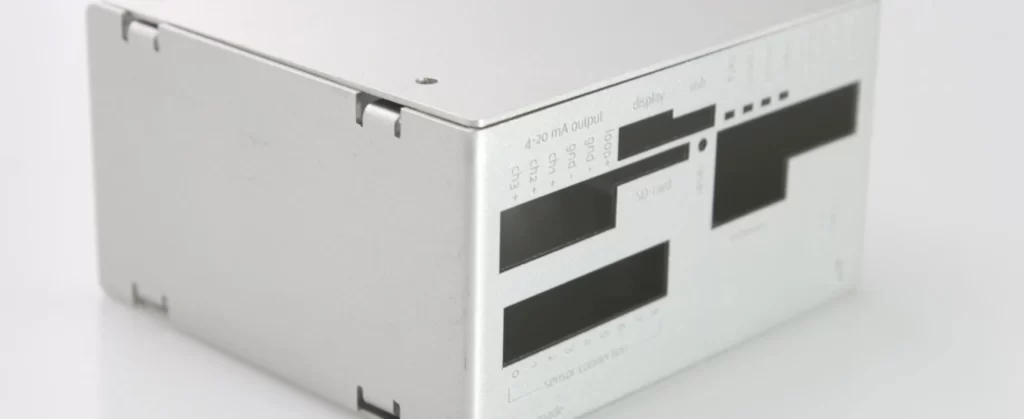
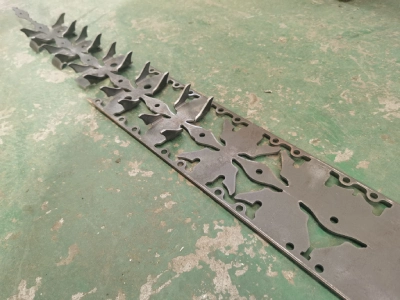
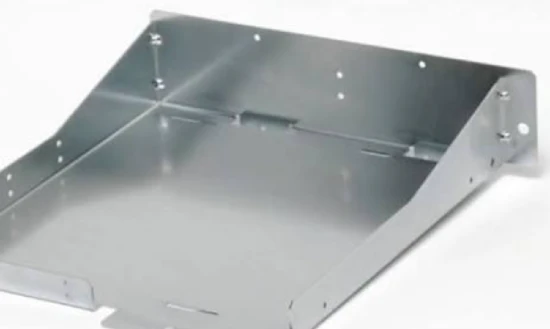
The combination of CNC fiber laser contour cutting and multi-axis press brake forming is the most flexible solution in the field of custom sheet metal fabrication. Fiber lasers utilize high-density photons to melt material along a narrow cut width, thereby minimizing thermal distortion and eliminating the need for custom hard dies (zero NRE).
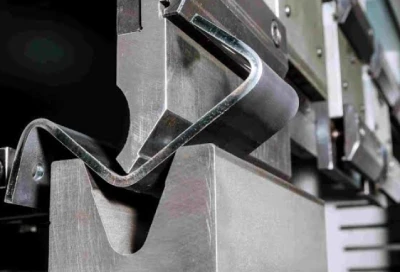
Subsequent forming operations on a CNC press brake rely on programmed air bending or bottoming sequences. Hydraulic or servo-electric backgages deliver high repeatability across variable bend radii and complex flange geometries. Advanced offline programming software instantly generates flat patterns based on precise material K-factors and bend allowances.
Although this “soft tooling” approach accelerates prototype iteration and eliminates upfront capital risks in sheet metal fabrication, its sequential processing nature results in longer cycle times and higher labor costs per unit, making the method prohibitively expensive for high-volume production.
Progressive and Compound Die Metal Stamping (High CapEx, Low Unit Cost)
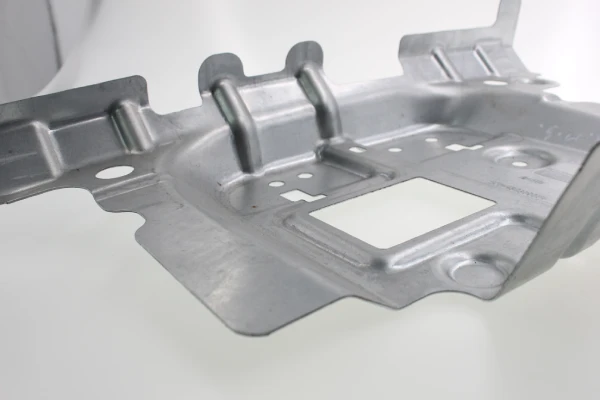
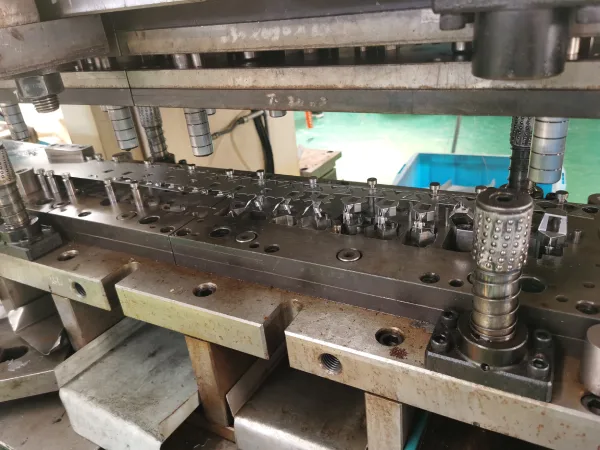
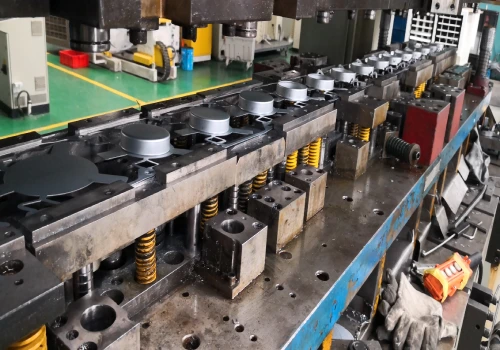
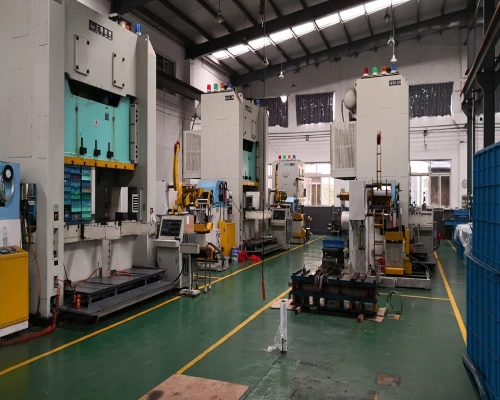
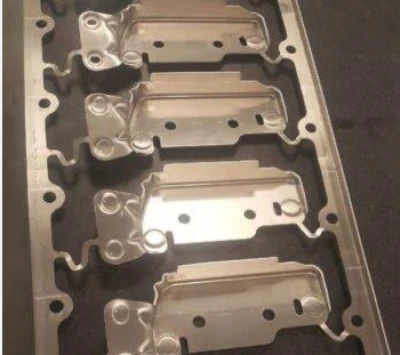
Progressive and compound die metal stamping technology has revolutionized high-volume precision sheet metal fabrication by transforming multi-step manual operations into automated, single-stroke stamping processes. High-speed mechanical or servo presses feed continuous metal coil into an engineered multi-station die, performing simultaneous blanking, piercing, notch-cutting, coining, and draw-forming within sub-second stroke cycles. By optimizing strip layout, custom dies maximize material utilization while maintaining tight geometric tolerances (±0.025 mm to ±0.05 mm) over millions of cycles.
Although progressive die design requires significant upfront tooling capital and a 6- to 12-week new product development (NRE) cycle, it significantly reduces unit manufacturing costs. For scalable custom sheet metal fabrication projects, the near-zero labor requirements and ultra-fast cycle times allow for rapid amortization of the initial investment in hard tooling.
The Financial Equation for Sheet Metal Fabrication: Quantifying Total Cost of Ownership (TCO)
Assessing the total cost of ownership in precision sheet metal fabrication requires balancing non-recurring engineering (NRE) costs against variable costs per unit. Accurate modeling of die amortization, equipment hourly rates, labor intensity, and material strip utilization is essential to determine the true long-term financial efficiency of each process.
Non-Recurring Engineering Costs (NRE) and Die Amortization
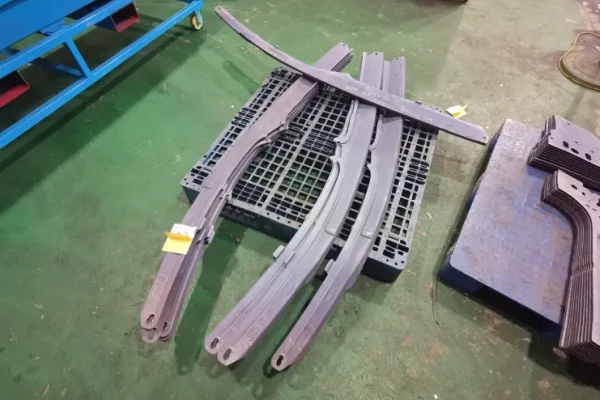
When evaluating the total cost of ownership for precision sheet metal fabrication, calculating the initial non-recurring engineering costs (NRE) is critical. The upfront NRE for laser cutting and press brake bending is negligible, limited only to CAM nesting and offline press brake setup costs. In contrast, continuous sheet metal stamping requires significant capital expenditure for custom tool steel dies. Depending on the complexity of the station, the drawing depth, and the required die life (e.g., D2 or SKD11 tool steel), costs typically range from $15,000 to over $80,000.
To establish true unit economics in scalable sheet metal fabrication, procurement managers must amortize this hard-die investment over the estimated annual usage (EAU). Over the long term, once the high initial capital expenditure (CapEx) is amortized, the cost per unit is only a fraction of a cent, creating a highly attractive financial model for high-volume projects.
Variable Cost per Unit: Cycle Time, Labor, and Material Utilization
Variable costs calculated per part reveal significant operational differences between soft-die workflows and high-speed hard-die processes in the field of custom sheet metal fabrication.
Laser cutting and CNC bending have high equipment hourly rates and require sequential manual operations, necessitating dedicated technicians for loading, vibratory deburring, and manual operation of the bending machine. In contrast, automated continuous stamping processes feed coil material continuously into high-tonnage mechanical presses, reducing the cycle time per unit to less than two seconds with minimal direct labor.
Furthermore, material utilization significantly impacts variable costs per unit. Nesting-based fiber laser cutting optimizes flat-panel layouts, while an engineering-optimized continuous stamping strip layout maximizes coil pitch efficiency and minimizes skeleton scrap. For high-volume sheet metal fabrication, the combined reduction in cycle time, labor hours, and raw material waste results in a significant reduction in the unit price.
Only 4 steps
online custom metal fabrication parts
Contact our experts team and experience the efficiency and economic benefits of digital metal fabrication services.
Upload Design Files
STL , STEP (.stp), IGES (.igs), (.ZIP), or PDF.
Also be a sample or an idea
Quote & Design Analysis
Instant factory quotes and DfM reports, the most reasonable solution.
Manufacturing Begins
Digital processes can initiate order tasks within 24 hours.
On-Time Delivery
Keeping delivery promises, approved by 3000+ Global Company buyers.
Establishing a Break-Even Point (BEP) Framework in the Sheet Metal Fabrication Process
To establish a robust break-even point framework in the field of precision sheet metal fabrication, precise mathematical modeling of the initial tooling investment and variable cost savings per unit is required. By comparing cumulative production expenditures, the exact production volume threshold at which a hard-tooling workflow outperforms a soft-tooling workflow can be determined.
Mathematical Modeling for Volume Transition
Establishing a mathematically rigorous break-even point (BEP) model is critical for optimizing capital allocation in custom sheet metal fabrication. The Director of Procurement must evaluate the precise break-even point at which the cumulative savings in unit variable costs offset the initial non-recurring engineering (NRE) expenses. The basic break-even equation is defined as:
Break-Even Volume (Q) = (Ctooling, stamping – Csetup, laser) ÷ (Vlaser/bending – Vstamping)
Here, Ctooling represents investment in hard tooling; Csetup covers soft tooling programming costs; Vlaser/bending denotes the sum of unit variable costs (including equipment hourly rates, direct labor, and sheet metal nesting efficiency); and Vstamping reflects the unit cost of automated coil feeding.
In addition to direct unit pricing, comprehensive financial modeling must also incorporate commissioning scrap rates, provisions for preventive tooling maintenance, and indirect costs associated with secondary deburring. In high-precision sheet metal fabrication processes, factors such as complex hole layouts or coining features can significantly increase manual bending time, thereby lowering the break-even volume Q and making progressive dies economically viable at significantly lower production thresholds.
Case Study Scenario: Evaluating Transition Thresholds
To illustrate the application of this economic framework in actual precision sheet metal fabrication, we use a medium-sized 304 stainless steel electrical mounting bracket as an example (2.0 mm thick, with six structural bends and twelve punch holes).
When using a flexible soft-tooling workflow (combining high-speed fiber laser cutting with a multi-axis CNC press brake), the initial non-recurring engineering (NRE) costs are negligible (Csetup = $350); however, due to labor costs associated with sequential processing and bending operations, the variable cost per unit remains as high as Vlaser/bending = $8.50.
On the other hand, switching to an automated continuous stamping production line—though requiring an initial tooling capital expenditure of Ctooling = $38,000—can reduce the variable cost per unit to Vstamping = $1.30 through sub-second single-stroke operations. Applying the break-even formula yields a key inflection point:
Q = ($38,000 – $350) ÷ ($8.50 – $1.30) = 5,229 units
For projects with an estimated annual usage (EAU) exceeding 5,500 units, the use of continuous stamping dies in sheet metal fabrication can amortize the total investment within the first year, thereby delivering a significant long-term improvement in profit margins.
Cost & Operational Metric | Soft Tooling Workflow (Fiber Laser + CNC Bending) | Hard Tooling Workflow (Progressive Die Stamping) |
Initial Tooling Cost (NRE) | $200 − $800 (Programming & Setup) | $15,000 − $80,000+ (Custom Hard Die) |
Production Lead Time (Setup to First Part) | 1 − 5 Days | 6 − 12 Weeks (Design, Machining & Tryout) |
Average Cycle Time per Part | 60 − 300 Seconds | 0.5 − 3 Seconds |
Achievable Standard Tolerance | ±0.127 mm (±0.005 in) | ±0.025 mm (±0.001 in) |
Typical Scrap Rate / Material Waste | 15% − 25% (Nesting skeleton loss) | 8% − 15% (Engineered strip layout) |
Direct Labor Intensity | High (Manual loading, bending & deburring) | Low (Automated coil-fed processing) |
Optimal Economic Volume (EAU) | 1 − 5,000 Units | 5,000 + Units |
Key DFM and Supply Chain Factors in Sheet Metal Fabrication Beyond Total Production Volume
Although production volume determines basic economic benefits, overall decision-making in the sheet metal fabrication process depends on key engineering and supply chain variables. The complexity of the geometry, feature tolerances, tooling lead times, and inventory carrying costs directly determine the long-term feasibility of manufacturing and risk management.
Design Complexity, Tolerances, and Secondary Processing of Sheet Metal Fabrication Components
Beyond pure EAU volume, part geometry and Design for Manufacturability (DFM) also determine the selection of the optimal sheet metal fabrication method.
Laser cutting and CNC press brakes can handle geometries of moderate complexity, but face technical limitations when managing close hole-to-bend proximity, micro-flanges, or tight feature-to-feature tolerances. Sequential bending of multi-axis geometries results in cumulative errors, often causing sheet metal fabrication part tolerances to exceed ±0.15 mm.
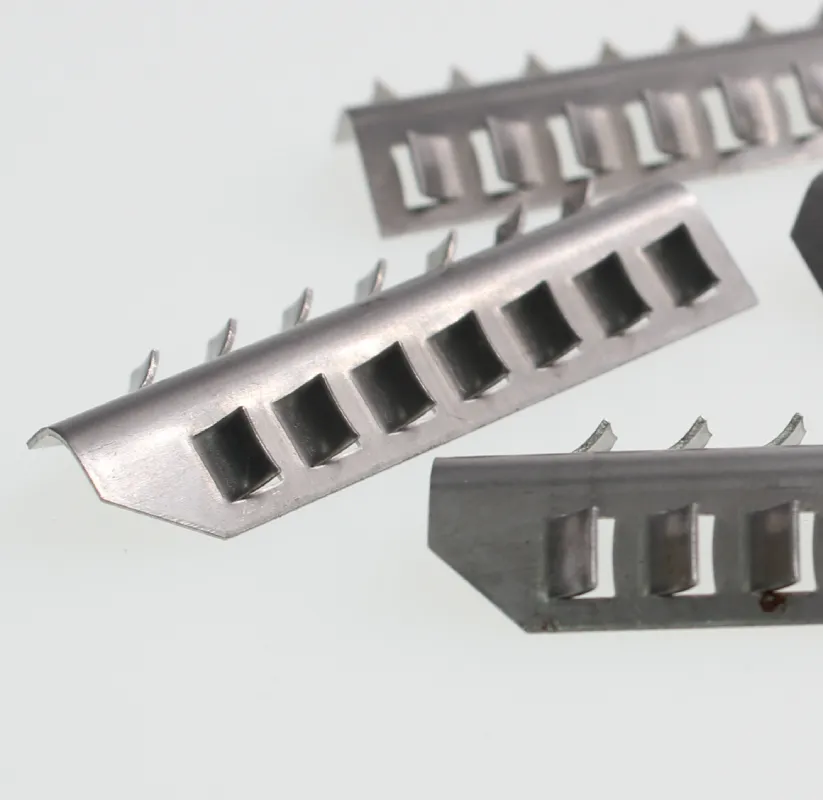
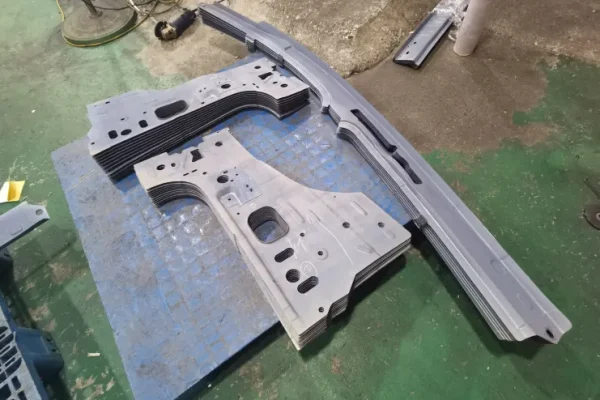
In contrast, progressive die stamping technology excels in precision sheet metal fabrication by integrating complex 3D forming, coining, draw-embossing, and high-density punching into a single rigid die set. Progressive die stamping consistently maintains tight tolerances (±0.025 mm to ±0.05 mm) and eliminates costly secondary operations such as manual deburring, reaming, or the individual insertion of hardware.
For complex sheet metal fabrication component designs, choosing progressive die stamping reduces overall unit costs by avoiding labor-intensive offline secondary operations, even at lower production volumes.
Lead Times, Inventory Carrying Costs, and Supply Chain Risk Mitigation
When building flexible and hard-die sheet metal fabrication supply chains, it is critical to evaluate lead times and working capital allocation. Fiber laser cutting and CNC bending enable unmatched time-to-market; since no hard dies are required, sheet metal fabrication prototypes can be produced and rapid batch deliveries completed within days. This agility enables original equipment manufacturers (OEMs) to implement “just-in-time” (JIT) production and minimize inventory carrying costs.
In contrast, the development of progressive dies for high-volume precision sheet metal fabrication requires a 6- to 12-week cycle for design, CNC machining, and die trial runs prior to initial production validation (FAI/PPAP). Procurement directors must strike a balance between the upfront die preparation cycle and long-term risk management.
Adopting a dual-track strategy—utilizing soft-tooling sheet metal fabrication processes to bridge the gap during initial market launch while progressive dies are being manufactured—protects assembly lines from the risk of stockouts while ensuring long-term, scalable unit economics.
Conclusion
To optimize the total cost of ownership in custom sheet metal fabrication, it is necessary to comprehensively evaluate production volume, part geometry, cumulative tolerances, and lifecycle projections.
Soft tooling processes, such as fiber laser cutting and CNC press brake forming, continue to offer significant advantages in rapid prototyping and low-volume projects, as they eliminate upfront non-recurring engineering (NRE) costs and provide flexibility in responding to engineering change orders. However, when production volumes exceed the mathematical break-even point, a transition to progressive die stamping becomes imperative. By amortizing the initial tooling capital, hard tooling can achieve cycle times of less than one second, exceptional dimensional repeatability, and significantly lower unit costs.
By partnering with an experienced sheet metal fabrication manufacturer early in the Design for Manufacturing (DFM) phase, the buyer can accurately calculate the trade-offs in unit costs, reduce supply chain risks, and efficiently allocate capital at every stage of the product lifecycle.