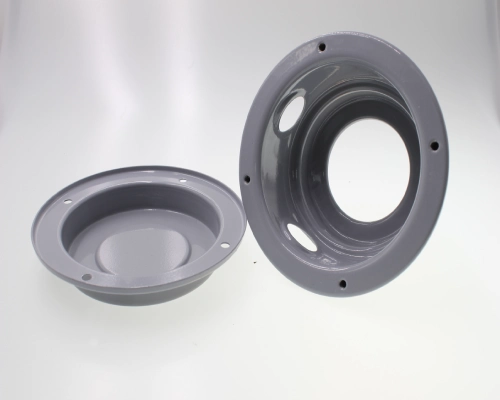


In the deep drawing of battery housings, microcracks in the corners are critical defects that compromise structural integrity. These cracks arise when local strain exceeds the material’s forming limits, directly weakening the housing’s ability to withstand mechanical impact and maintain airtightness.
To systematically eliminate this risk, one cannot rely on a single adjustment alone; instead, it is necessary to start from the mechanical fundamentals of material flow and comprehensively optimize the constraint strategy and lubrication scheme for draw beads, thereby achieving precise control over metal flow.
This article will explore in depth how this systematic engineering approach can ensure the stability and reliability of the deep drawing process for battery housings.
Key Challenge: Maintaining Structural Integrity at the Fillet of the Battery Housing
For functional components such as custom battery housings, the structural integrity of the fillet in deep-drawn corners is a fundamental prerequisite for their in-service performance. The danger of microcracks in this area lies precisely in their concealment—they typically originate at the microscopic scale and are difficult to detect through routine visual inspection, yet they are sufficient to act as stress concentration points. During subsequent use or under fatigue loading, these cracks significantly reduce the effective load-bearing cross-section of the housing, ultimately leading to structural failure.
From a mechanical perspective, these cracks originate from local peaks in principal strain caused by the superposition of in-plane strain and thickness reduction in this region. Once these peaks exceed the critical value defined by the battery housing material’s forming limit curve, microscopic damage will irreversibly initiate and propagate.
Therefore, understanding and controlling this failure mechanism serves as the theoretical foundation for developing effective process countermeasures.
Analysis of the Causes of Microcracks in Deep-Drawn Battery Housings
To resolve microcracks in the corners of deep-drawn battery housings, it is necessary to systematically examine the entire chain of process variables, ranging from material properties to die design and processing. This defect typically stems from a combined failure resulting from the interaction of multiple factors, including the material’s forming limit, stress state, and friction conditions. The following analysis will examine the root causes from three core dimensions.
Selection of Battery Housing Material and Its Forming Limit
During the deep drawing of battery housings, the material’s inherent formability serves as the first line of defense against cracking. Alloys of different grades and conditions exhibit significant variations in their work hardening index and maximum drawing ratio.
If the selected battery housing material has an insufficient coefficient of anisotropy, or if its elongation cannot meet the demands of severe bidirectional stretching at the R-corner, the local principal strain will rapidly approach and exceed its formability limit curve.
At the microstructural level, this leads to impeded lattice slip, with dislocation accumulation causing stress concentration that ultimately releases as microcracks. Therefore, failing to ensure a proper match between the material’s forming limits and the part’s geometric features constitutes a fundamental design flaw that leads to failure.
Interaction Between Blank Holder Force and Draw Bead Design
Blank holder force (BHF) and draw beads together constitute a “valve system” that controls material flow. If the blank holder force is too low, the flange material is prone to wrinkling; if it is too high, it significantly increases the resistance to flow into the die, exacerbating thinning in the R-corner region.
The geometric parameters of draw beads—particularly their fillet radius and height—directly determine the magnitude and distribution of the resistance force. An improper draw bead layout disrupts material flow, leading to uneven circumferential strain distribution and subjecting corner regions to additional tangential tensile stress.
This mechanical imbalance directly contributes to the formation of microcracks in the corners of deep-drawn battery housings, where deformation is most severe.
Lubrication Failure
In deep drawing, lubrication is not a secondary process but a critical variable that determines success or failure. Its function is not only to reduce temperature but also to establish a stable, controllable friction coefficient environment.
When extreme-pressure additives are insufficiently active, lubricant application is uneven, or the oil film breaks down at high temperatures, localized dry friction or even material adhesion will occur between the die and the sheet metal. This leads to:
A sharp increase in deformation resistance.
Severe obstruction of battery housing material flow.
Localized heat buildup.
These factors combine to significantly increase the shear stress in the corner regions of the custom battery housing, causing the metal—already at a critical state—to rapidly exceed its fracture strength and induce microcracks.
Are you looking for reliable & cost-effective
China metal fabrication manufacturer
More than 150,000 OEM metal fabrication products delivered to 5,000+ global buyers.
And benefit from it!
Comprehensive Solution: From the Perspective of Battery Housing Manufacturing
To address the issue of microcracks in the corners of deep-drawn battery housings, a systematic approach requires the synergistic interaction of materials, dies, and processes. The core of the solution lies in precisely controlling material flow and stress states. Specific measures are outlined below across three engineering dimensions.
Strategic Selection of Battery Housing Materials for Deep-Drawing Performance
From the perspective of battery housing manufacturing, the key to material selection lies in balancing strength and formability. Priority should be given to specialized deep-drawing materials with high work-hardening indices and anisotropy coefficients, such as aluminum alloys 3003-O or 5052-O. Their stable O-state (fully annealed) microstructure provides an excellent ultimate drawing ratio. For high-strength solutions, HSLA steel grades may be evaluated, but their forming limit curves must be rigorously verified.
Prior to mass production, material properties should be quantified through tensile tests and cup-crush tests to ensure that the elongation matches the thinning rate at the part’s R-corner, thereby reducing the risk of microcracks at the source.
Optimizing Die Parameters to Control Material Flow
Controlling material flow is the core process method for addressing microcracks in the corners of custom battery housings. By optimizing the layout, fillet radius, and height of draw beads through CAE simulation—including the use of variable-height or segmented draw beads—differential resistance can be applied in the corner regions to balance circumferential material flow.
At the same time, the blank holder force (BHF) curve must be precisely set to minimize flow resistance as much as possible while preventing wrinkling. Furthermore, appropriately increasing the radius of the punch and die fillets can effectively disperse local peak principal strains, steering the strain path away from the danger zone of the forming limit curve and ensuring that deformation is distributed more uniformly across the entire deep-drawn battery housing.
Establishing a Robust Lubrication Scheme
The lubrication strategy directly determines the stability and consistency of the coefficient of friction. As an experienced battery housing manufacturer, Supro has abandoned generic lubricants in favor of deep-drawing oils specifically designed for deep drawing. These oils must possess excellent extreme-pressure properties and thermal stability to maintain a continuous oil film under high pressure and high temperature conditions. Furthermore, we implement a metered application system to ensure uniform lubricant coverage on the surface of each batch of sheet metal.
For multi-pass deep drawing, a dual-layer lubrication strategy or the use of sheet metal with a lubricating coating may be considered. In mass production of battery housings, we monitor lubricant viscosity and cleanliness through in-line monitoring and periodic spot checks to ensure consistent friction conditions throughout the entire production cycle and eliminate sporadic cracking caused by fluctuations in lubrication.
Process Validation and Quality Assurance for Battery Housings
Process validation and quality assurance are the cornerstones of ensuring the long-term stability of the deep-drawing process for battery housings. Through systematic inspection and monitoring methods, this phase transforms engineering solutions into repeatable and traceable production capabilities. The following sections address this from the perspectives of inspection and process control.
Non-Destructive Testing (NDT) for Microcrack Detection
Given the concealed nature of microcracks in the corners of deep-drawn battery housings, effective non-destructive testing (NDT) methods must be employed for piece-by-piece or sampling screening. Penetrant testing is a cost-effective method for detecting surface-opening defects; its high sensitivity can clearly reveal fine cracks in the R-corner areas. For more demanding applications, eddy current testing can rapidly detect near-surface cracks without the need for a coupling agent, making it suitable for integration into production lines.
For 100% inspection requirements, automated optical inspection systems can be evaluated, utilizing high-resolution cameras and image algorithms to identify surface anomalies. When selecting NDT methods, detection sensitivity, efficiency, and cost must be comprehensively considered, and clear acceptance criteria must be established in accordance with PPAP requirements to ensure that only defect-free battery housings proceed to the next process step.
Process Parameter Monitoring and Recording
The key to achieving process robustness lies in the real-time monitoring and data-driven management of critical process parameters. In deep-drawn battery housing production, core variables such as the blank holder force (BHF) curve, stamping speed, temperature, and lubricant flow rate must be continuously recorded. By setting reasonable upper and lower control limits and establishing a statistical process control system, parameter drift trends can be detected in a timely manner, allowing for intervention before defects occur.
Comprehensive parameter records not only provide a data foundation for process capability analysis but are also essential for achieving production traceability and submitting PPAP documentation. This data-driven monitoring system transforms process knowledge into standardized operating procedures, ensuring consistent quality for every batch of custom battery housings.
Conclusion
To eliminate microcracks in the corners of deep-drawn battery housings, the material, die, and process must be viewed as an integrated, interactive system. Through validation, systematically optimizing draw bead constraints to balance material flow and establishing a robust lubrication scheme to maintain a stable coefficient of friction can fundamentally control the strain path in the R-corner region, ensuring it remains within the safe range of the forming limit curve at all times.
Ultimately, supplemented by rigorous non-destructive testing and process monitoring, this systematic approach transforms process stability into quantifiable quality improvements, effectively enhancing the structural integrity and fatigue life of custom battery housings.
From an engineering perspective, this represents a reliable shift from “post-hoc inspection” to “process design and prevention,” directly reducing overall manufacturing costs and enhancing supply chain reliability.
Supro is a professional custom battery housing manufacturer. Leveraging advanced equipment, extensive manufacturing experience, and a dedicated engineering team, we provide perfect custom battery housing solutions to over 3,000 companies worldwide, along with genuine manufacturer quotes.
We deliver a wide range of products efficiently and on time. From product design and rapid sheet metal prototype fabrication to mass production, we provide professional technical support and exceptional quality.
Supro offers one-stop manufacturing solutions and highly cost-competitive product supply! For technical specifications or inquiries regarding OEM partnerships, please contact our engineering team.