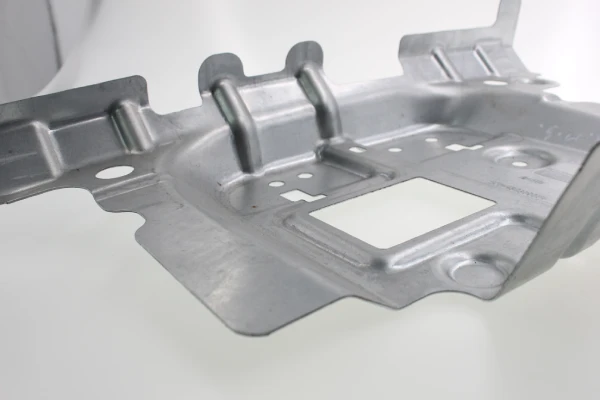
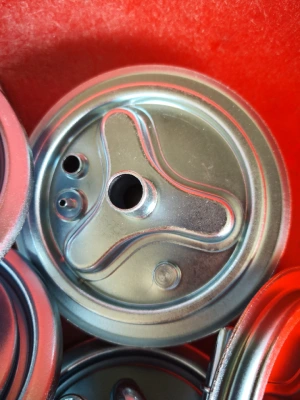

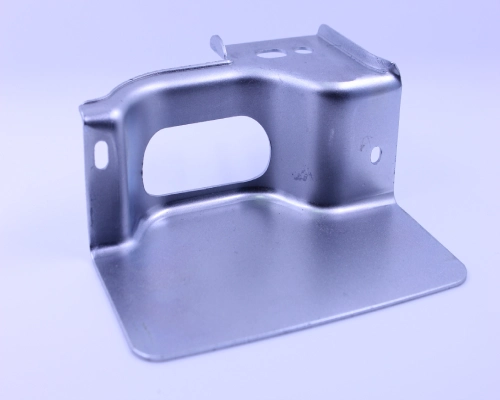
Finding a partner for high-volume metal parts production is a critical capital expenditure (CapEx) decision—not merely a simple price comparison. In the field of progressive die stamping, custom dies represent a significant upfront investment that directly determines the stability of the entire production lifecycle. Partnering with unqualified suppliers often leads to accelerated die wear, uncontrolled dimensional drift (such as microcracks or springback), and ultimately results in costly production line downtime. For procurement professionals, the truly important metric is total cost of ownership (TCO).
To mitigate supply chain risks and ensure that progressive die stamping parts maintain tight tolerances over millions of stamping cycles, buyers must implement an engineering-driven audit process.
This article provides a technical checklist for evaluating progressive die stamping manufacturers and offers an in-depth analysis of key metrics—with a focus on internal die infrastructure, precise press tonnage matching, and strict adherence to PPAP and FAI documentation. By adopting this analytical framework, procurement teams can confidently identify qualified suppliers capable of delivering uncompromising precision.
Evaluate a progressive die stamping manufacturer’s in-house die manufacturing capabilities
The success of any custom progressive die stamping project hinges on the die itself. Relying on outsourced die manufacturers can lead to significant delivery delays and tolerance risks. The buyer must verify that the company has a robust in-house die manufacturing system to ensure consistent precision and strict control over the product lifecycle.
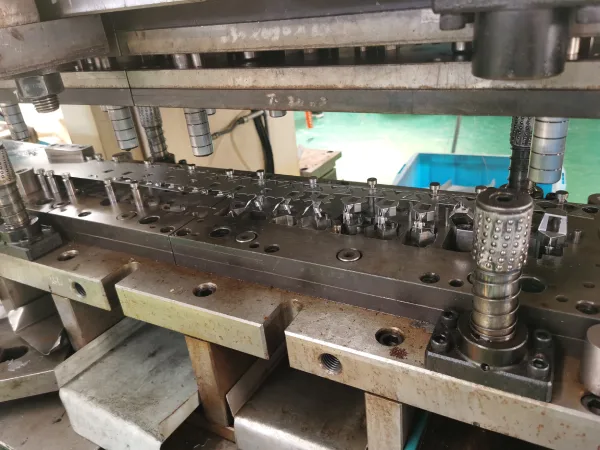
Expertise in Progressive Stamping Die Design and Simulation
Tier-1 suppliers do more than simply manufacture dies; they eliminate potential manufacturing defects through engineering design before cutting the steel. During the rigorous DFM (Design for Manufacturability) phase, leading manufacturers utilize advanced finite element analysis (FEA) simulation software, such as AutoForm, to predict material behavior. This “digital twin” approach is an absolute prerequisite for successful progressive die metal stamping; it enables engineers to precisely calculate springback, optimize strip layout, and prevent microcracks in high-strength alloys.
By conducting comprehensive virtual die trials, manufacturers can significantly reduce the number of physical iteration cycles. For procurement teams evaluating any progressive die stamping partner, requiring proof of upfront simulation validation ensures higher material utilization and tighter tolerances. Ultimately, true expertise in progressive metal stamping means eliminating the trial-and-error process and ensuring that complex die geometries are fully validated before capital is invested.
Strategic Advantages of In-House Die Maintenance (MRO)
Even the highest-quality dies are subjected to immense mechanical stress, and over time, issues such as wear, punch blunting, and tolerance drift inevitably arise. For this reason, dedicated in-house MRO (maintenance, repair, and overhaul) services have become an indispensable evaluation criterion when selecting a progressive die stamping manufacturer.
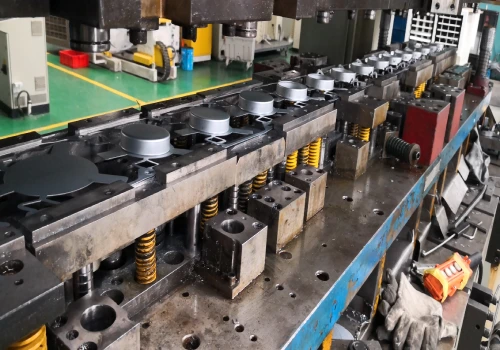
When a supplier relies on external tooling shops for edge grinding, sensor replacement, or blade repair, what would otherwise be minor maintenance tasks can escalate into catastrophic production delays. An in-house tooling shop equipped with wire-cut EDM machines and CNC grinders ensures that corrective measures can be taken immediately. By centralizing all MRO operations within a single facility, a progressive die stamping plant can guarantee consistent repeatability between strokes while effectively eliminating logistics delays.
For buyers, selecting a progressive die stamping manufacturer capable of providing rapid on-site die maintenance services directly translates to zero production line downtime and ensures a reliable, long-term supply chain.
Verify the Progressive Die Stamping Manufacturer’s Equipment Specifications and Production Capacity
Un éxito custom progressive die stamping project requires precise equipment matching. The procurement team must review the actual press tonnage, table size, and automation integration based on the part’s yield strength. Insufficient equipment specifications will inevitably lead to stroke bottlenecks, premature die wear, and inadequate production capacity.
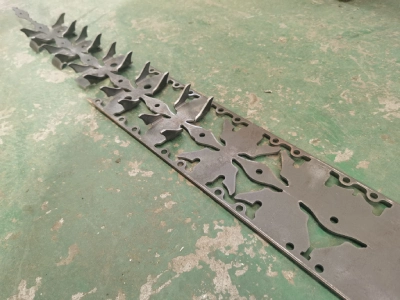
Limitaciones de tonelaje y tamaño de la prensa
When evaluating a progressive die metal stamping shop, the buyer must rigorously assess the manufacturer’s press tonnage configuration based on the specific part geometry and material yield strength. If the press table size cannot accommodate complex multi-station dies, simply having high-tonnage equipment is far from sufficient.
A reliable progressive die stamping manufacturer will actively match the closing height and tonnage to the precise blanking, punching, and forming force requirements of the strip material. Using a press with insufficient tonnage can result in destructive reverse tonnage (penetration impact), which causes die component fractures and severely compromises long-term dimensional repeatability. Conversely, a properly matched mechanical or servo press ensures consistent kinetic energy transfer.
For high-strength alloys, procurement teams must verify that the supplier’s progressive die stamping presses have the necessary frame rigidity and platen dimensions to prevent deflection over millions of stamping cycles.
Automation Integration in Progressive Metal Stamping
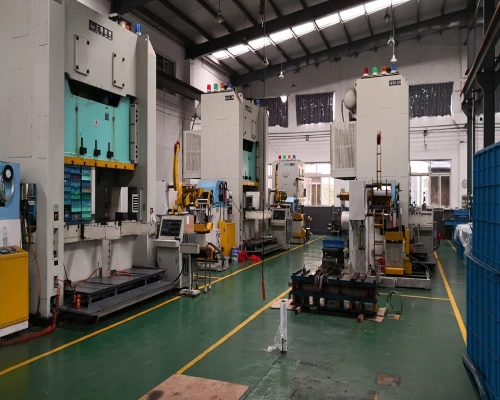
True efficiency in high-volume production extends far beyond the stamping press itself; it depends entirely on seamless automation integration. To achieve the highest strokes per minute (SPM) in high-speed progressive die stamping, Tier 1 suppliers require automated coil-handling systems, including precision servo coil feeders and heavy-duty straighteners. These peripheral devices ensure smooth and error-free strip feeding and eliminate memory deformation in the coil before the material enters the die.
Without a synchronized automation system, manual intervention disrupts the continuous rhythm required for stable progressive die estampado de metal, directly leading to increased cycle times and unit costs.
In addition, automated scrap conveyors and sensors integrated into the dies (such as misfeed detection) are critical process safeguards. By auditing these automated feeding lines, the purchaser can verify whether the manufacturer has the technical infrastructure to sustain high-speed, unattended production while effectively eliminating catastrophic collisions involving progressive stamping dies.
Rigorous Quality Documentation in Progressive Die Stamping Production: PPAP and FAI
Verbal assurances of high quality alone are insufficient to meet stringent OEM compliance requirements. In the field of progressive die metal stamping, buyers must demand rigorous, data-driven validation. Requiring comprehensive PPAP and FAI documentation ensures statistical process control (SPC), verifies Cpk metrics, and guarantees absolute traceability between batches.
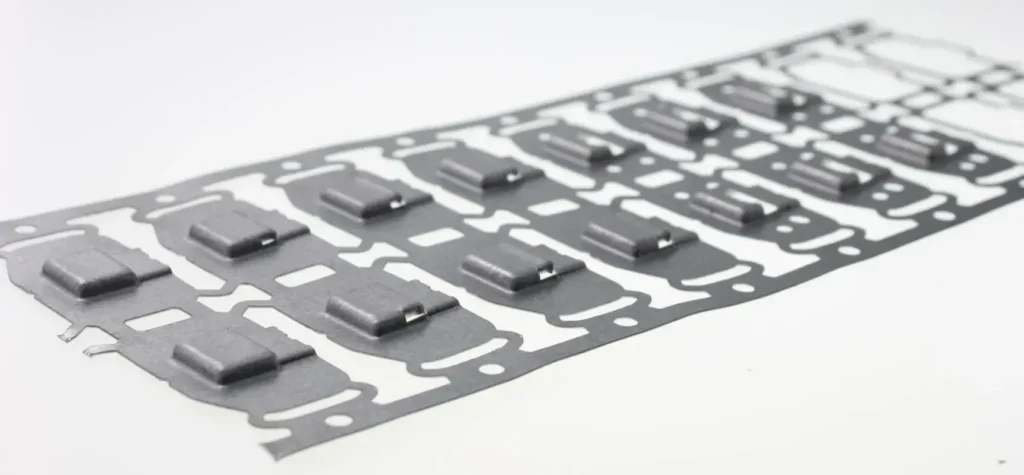
Performing First Article Inspection (FAI) During the Progressive Die Stamping Production Process
Before commencing any high-volume production, conducting a rigorous First Article Inspection (FAI) is critical for validating the entire progressive die stamping process setup. Tier-1 suppliers utilize advanced coordinate measuring machines (CMMs) to verify that the first batch of lower die samples strictly conforms to complex geometric dimensions and tolerances (GD&T) requirements. This process involves more than just dimensional inspection; it is designed to establish an engineering baseline.
In custom progressive die stamping, comprehensive FAI documentation must actively verify die accuracy and confirm the absolute absence of edge burrs, material thinning, or stress-induced microcracks. For procurement professionals, a detailed FAI report provides irrefutable evidence that the supplier’s die geometry has been stably established. If a manufacturer treats this verification step carelessly, subsequent progressive metal stamping batches will inevitably exhibit cumulative dimensional deviations, thereby posing a risk of severe assembly failure.
Addressing the Production Part Approval Process (PPAP)
To ensure long-term supply chain security, the purchaser must require the implementation of a Level 3 Production Part Approval Process (PPAP). This data-intensive documentation demonstrates that the progressive die stamping process is statistically viable, repeatable, and ready for large-scale mass production. Leading metalworking suppliers will provide detailed Process Failure Mode and Effects Analysis (PFMEA) reports and robust control plans that clearly explain how they have engineered out risks such as springback or warpage over millions of cycles.
Además, true progressive die metal stamping experts will demonstrate high Cpk and Ppk capability indices, supported by proactive CAPA (Corrective and Preventive Action) protocols. For procurement teams, reviewing these documents is essential. A validated PPAP documentation package ensures that the progressive die stamping manufacturer relies on rigorous statistical process control rather than operators’ rule-of-thumb judgments, thereby reinforcing a zero-defect production environment.
Solo 4 pasos
piezas de fabricación de metal personalizadas en línea
Póngase en contacto con nuestro equipo de expertos y experimente la eficiencia y los beneficios económicos de los servicios de fabricación digital de metales.
Subir archivos de diseño
STL, STEP (.stp), IGES (.igs), (.ZIP) o PDF.
También sea una muestra o una idea.
Cotización y análisis de diseño
Cotizaciones instantáneas de fábrica e informes DfM, la solución más razonable.
Comienza la fabricación
Los procesos digitales pueden iniciar tareas de pedidos dentro de las 24 horas.
El tiempo de entrega
Cumplir las promesas de entrega, aprobadas por más de 3000 compradores de empresas globales.
Audit of the Progressive Die Stamping Manufacturer’s Quality Management System (QMS)
A framed certificate alone does not guarantee precision. For high-volume progressive metal stamping, the buyer must audit the actual implementation of the quality management system. A robust framework requires the implementation of systematic defect prevention, strict material traceability, and proactive and effective Corrective and Preventive Action (CAPA) execution to ensure repeatable zero-defect performance over millions of stamping cycles.

Distinguishing Between ISO 9001 and IATF 16949 Compliance
While ISO 9001 provides a basic framework for quality control, Tier 1 progressive die stamping manufacturers typically adhere to the more stringent IATF 16949 standard. This distinction is critical for OEM procurement teams. ISO 9001 focuses on general process compliance, whereas IATF 16949 requires the implementation of proactive defect prevention and variation control throughout the supply chain. Suppliers adhering to IATF principles proactively apply core automotive tools—such as APQP, FMEA, and MSA—to eliminate risks such as warping or microcracks through engineering design before actual production begins.
When procuring high-volume progressive die stamping parts, buyers must require suppliers to possess this higher level of systematic control capability. Partnering with progressive die metal stamping manufacturers that strictly enforce these automotive-grade methodologies ensures exceptional part-to-part consistency, thereby effectively eliminating long-term tolerance drift issues.
Trazabilidad y cumplimiento de materiales
Absolute material traceability is the cornerstone of supply chain security, and its significance extends far beyond simple RoHS or REACH environmental compliance requirements. During high-speed progressive die stamping, subtle variations in the metallurgical properties of steel coils—such as inconsistencies in yield strength or tensile properties—can lead to severe springback or premature die wear. Leading manufacturers maintain granular traceability across batches, linking each finished part directly to the original mill test report (MTR) and specific heat treatment lot number.
In the event of an assembly failure, a certified progressive die stamping manufacturer can pinpoint the exact steel coil batch within minutes, thereby preventing large-scale OEM recalls. For procurement professionals, auditing this closed-loop tracking system is essential. A progressive metal stamping partner capable of seamlessly integrating rigorous material certification processes can protect your brand from devastating legal liability resulting from the use of non-compliant alloys.
Conclusión
Ultimately, selecting a manufacturing partner for high-volume metal parts is, at its core, a strategic risk mitigation effort. Procurement teams must look beyond initial unit-price considerations and rigorously audit the supplier’s entire engineering ecosystem. Truly reliable progressive die stamping manufacturers eliminate hidden lifecycle costs by maintaining robust in-house die infrastructure, precisely matching press tonnage to material yield strength, and executing data-driven three-tier PPAP validation.
Compromising on these critical technical metrics will inevitably lead to accelerated die wear, uncontrolled dimensional drift, and even catastrophic production line downtime. By strictly enforcing this checklist, procurement teams can identify qualified stamping suppliers and ensure they maintain zero-defect repeatability over millions of progressive die metal stamping cycles.
Partnering with Level 1 progressive die stamping experts ensures complete process transparency, ultimately safeguarding your global supply chain and reducing your total cost of ownership (TCO).
For technical specifications, customized project solutions, or OEM partnership inquiries, please contact Supro immediately. Our professional engineering team is ready to provide you with tailored application solutions.